In short
- Jaw plates, the cone's mantle and concave, and screen mesh are consumed by the rock. Belts, idlers and bearings wear more slowly but stop the plant just as completely.
- Liner life is counted in tonnes crushed, not months, and varies several-fold with the rock. One reported granite case ran 20,000 to 30,000 tonnes per set of jaw plates.
- Wear shows in the product first: the closed side setting opens, the grading coarsens, shape worsens and screens blind or tear.
- A liner ordered on the day it fails can take weeks. Under our per-tonne rate the wear parts are our cost and are stocked at the plant.
A crusher loses a little steel to every tonne it breaks. The parts inside the crushing chamber are designed to be consumed: jaw plates, the cone's mantle and concave, the screen mesh. The question is never whether they wear. It is whether the replacement is on the shelf when they do.
The costly part is not the steel. It is the grading that drifts for a fortnight before anyone changes the plate, and the weeks a plant can stand if the spare has to be ordered.
What wears and why
Crusher liners are cast in manganese steel for one odd property. It is fairly soft when new and hardens under impact: the working face toughens as rock hammers it, while the metal beneath stays ductile enough not to crack.
It suits abrasion less well. Where rock slides across the steel without hitting it hard, the surface never hardens properly and is ground away. So two things decide how fast a liner goes: how hard the rock hits, and how much free silica it carries. Quartz-rich rock scratches steel in a way that calcite-rich rock does not. How basalt, granite, sandstone and limestone behave at the crusher takes that further.
Jaw plates
A jaw has a fixed plate and a swing plate, both toothed. Wear concentrates low in the chamber, where the rock is smallest and the squeeze is hardest. Most plates are symmetrical so that they can be turned end for end, and good practice is to rotate them on a schedule so that the teeth wear evenly. A plate turned late has already lost its profile at one end, and the tonnes it would have given are gone.
Cone mantle and concave
In a cone the wearing pair is the mantle, which gyrates, and the concave or bowl liner, which is fixed. They are normally changed together. The trouble is uneven wear. A cone that is trickle-fed, or fed to one side, wears a pocket into its liners. The pocket changes the shape of the chamber, and from then on the machine cannot hold its setting or its product shape however the operator adjusts it. Steady, full feed is the cheapest liner-life measure there is, and a three-stage plant is laid out to give it.
Screen mesh, belts, idlers and bearings
Woven wire mesh is cheap, gives the most open area and the sharpest cut, and wears out quickest. Polyurethane and rubber panels cost more and last far longer under abrasive rock, but they have less open area and can blind in damp, sticky feed.
Belts wear at the loading points and along the edges when they track off-centre. Idlers seize when dust gets past the seals, and a seized idler cuts the belt dragging over it. Bearings fail from dirty grease or a missed interval more often than from age. Each stops the plant as surely as a cracked jaw plate.
Wear changes the product before it stops the plant
The closed side setting is measured between the liners. As they wear, the gap opens with nobody touching the adjustment, and the product coarsens. More oversize returns from the screen, the recirculating load climbs, and finished tonnes fall while the plant sounds as busy as ever.
Shape goes next. A worn chamber nips rock less cleanly, more slabby pieces get through, and the flakiness index on the 20 mm and 10 mm creeps up. On the screens, worn wire stretches and the apertures grow, which lets oversize into a single-size stockpile. Blinded mesh does the opposite and sends good product back round. A sieve analysis that has drifted coarse over ten days is telling you about the liners or the mesh.
| Part | What wears it | Sign it is due | What happens if you run it on |
|---|---|---|---|
| Jaw plates | Impact and abrasion, worst low in the chamber | Teeth flattened; setting needs closing often | Coarse, slabby product; plate cracks or wears through |
| Cone mantle and concave | Compression and abrasion; uneven feed | Setting will not hold; pocketed liner | Flaky product; liner works loose; damage to head or bowl |
| Screen mesh or panels | Abrasion; impact on the top deck | Oversize in single-size stockpiles; broken wires | Failed gradings; a torn panel contaminates a stack |
| Belts and idlers | Impact at loading points; mistracking; dust in idler seals | Worn cover, frayed edges; rollers not turning | Belt tears, or a seized roller cuts it |
| Bearings | Dirty grease; a missed interval | Heat, noise, vibration | Shaft or housing damage and a long stoppage |
How long plates and liners last
It depends on the rock, by a wide margin. Life is counted in tonnes crushed, not in weeks, and the same plate can give several times the tonnage in soft, low-silica rock that it gives in hard, abrasive rock.
Published figures are scarce. The one case we can cite is a trade-press report from a granite quarry in Scotland working hard, abrasive rock. It was getting 20,000 to 30,000 tonnes from a set of jaw plates, and 50,000 to 55,000 tonnes after changing to a different tooth profile. That is one quarry and a supplier-linked account. It does not say what your rock will do, and we found no measured Indian figure fit to print.
Keep your own record: tonnes across the weighbridge between plate changes, by quarry. After two changes you have a number that beats any brochure.
Stocking, lead time and who carries the cost
Liners are heavy castings, specific to the machine. One ordered on the day it fails can take weeks to arrive, and we plan on three weeks to get a liner shipped in to a project site.
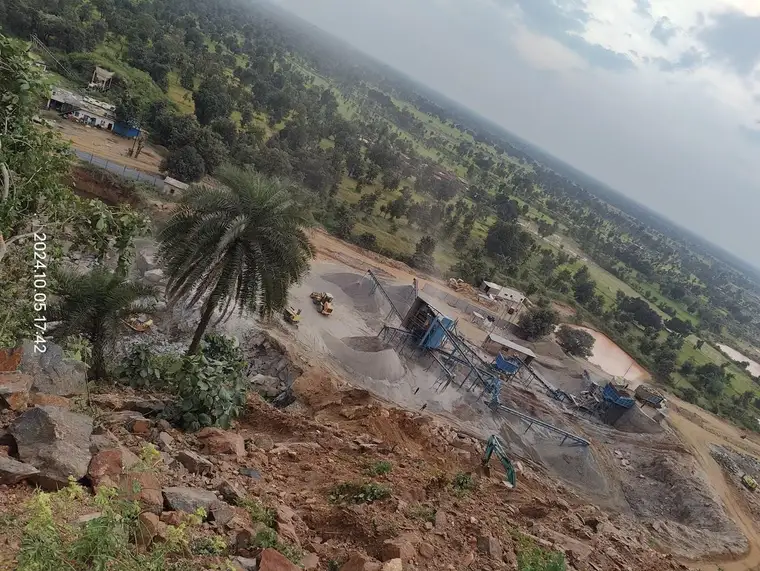
That lead time is why, on our crushing contracts, wear parts sit inside the per-tonne rate and on a shelf at the plant. Jaw plates, cone liners, screen mesh, belts and bearings are stocked on site, and the fitter and electrician are there too, so a wear failure costs hours and most stoppages are a shift. We are paid per tonne of finished material, so a plant waiting for a casting earns us nothing. What sits inside a per-tonne crushing rate sets out the rest.
If you own the plant, the same logic applies with your money. Hold a full set for each crusher and re-order when a set is fitted, not when it is worn. Hard basalt and granite use them faster than sandstone does, so budget by the rock. And if the plant is not holding its output and nobody on site can say why, handing the operation to a crew that does nothing else is worth pricing.
Standards and sources
- Jaw plate life: a single supplier-linked trade press report (KHL and World Highways) from a granite quarry in Scotland. One case, not a general figure
- Wear part stocking, site crew, lead time and contract terms: SM Infra's own operating record
Your contract and its technical schedules override anything written here. Check the clause before you build to it.