In short
- The offset at the bottom of a straight hole is its depth multiplied by the tangent of the angular error. Two degrees over 10 m is about 0.35 m.
- There are three separate errors: the collar in the wrong place, the mast set at the wrong angle, and the bit deflecting inside the rock. They add.
- Too much burden at the toe leaves a toe and oversize. Too little is a recognised cause of flyrock.
- Control costs little next to the consequences: marked collars, an angle check at every set-up, holes measured before charging, and a bad hole redrilled, not accepted.
- Oversize is paid for twice, once at the rock breaker and again in the hours the primary jaw stands bridged.
Two degrees is nothing. Stand beside a drill mast that is two degrees off plumb and you will not see it. The rock notices, because an angle becomes a distance once it has some depth to work with, and a blast hole gives it plenty.
The answer is trigonometry. A hole that is 2 degrees off line moves sideways by about 3.5 per cent of its length, so at the bottom of a 10 m hole it is 0.35 m from where the design put it. The charge in that hole then has more rock to move than it was designed for, or less. Both are trouble, and the first kind arrives at the crusher as oversize.
Three kinds of error
- Collar position. The hole starts in the wrong place: the mark was kicked away, or the rig could not stand where it needed to. The error is the same at the top of the hole and the bottom.
- Alignment at set-up. The hole starts in the right place and points the wrong way, in angle or in direction. The error is nil at the collar and grows in a straight line with depth.
- In-hole deflection. The hole starts right and points right, and then the bit is pushed aside by the rock or the string bends. It can grow faster than depth does, and it cannot be seen from the bench.
A real hole can carry all three, and they do not reliably cancel.
The geometry
For a straight hole the sum is short: the offset at the toe equals the depth multiplied by the tangent of the angular error.
| Hole depth | 1 degree off | 2 degrees off | 3 degrees off |
|---|---|---|---|
| 6 m | 0.10 m | 0.21 m | 0.31 m |
| 10 m | 0.17 m | 0.35 m | 0.52 m |
| 15 m | 0.26 m | 0.52 m | 0.79 m |
Depth × tan(angle), with tan 1° = 0.0175, tan 2° = 0.0349 and tan 3° = 0.0524. Set-up error only. Deflection inside the rock comes on top.
Read down the middle column. The same two degrees that costs 0.21 m on a 6 m hole costs 0.52 m at 15 m, two and a half times as much, which is one reason the drill has to suit the bench. Choosing between DTH, top hammer and wagon drill covers which machines hold their line at depth.
What it does to the burden at the toe
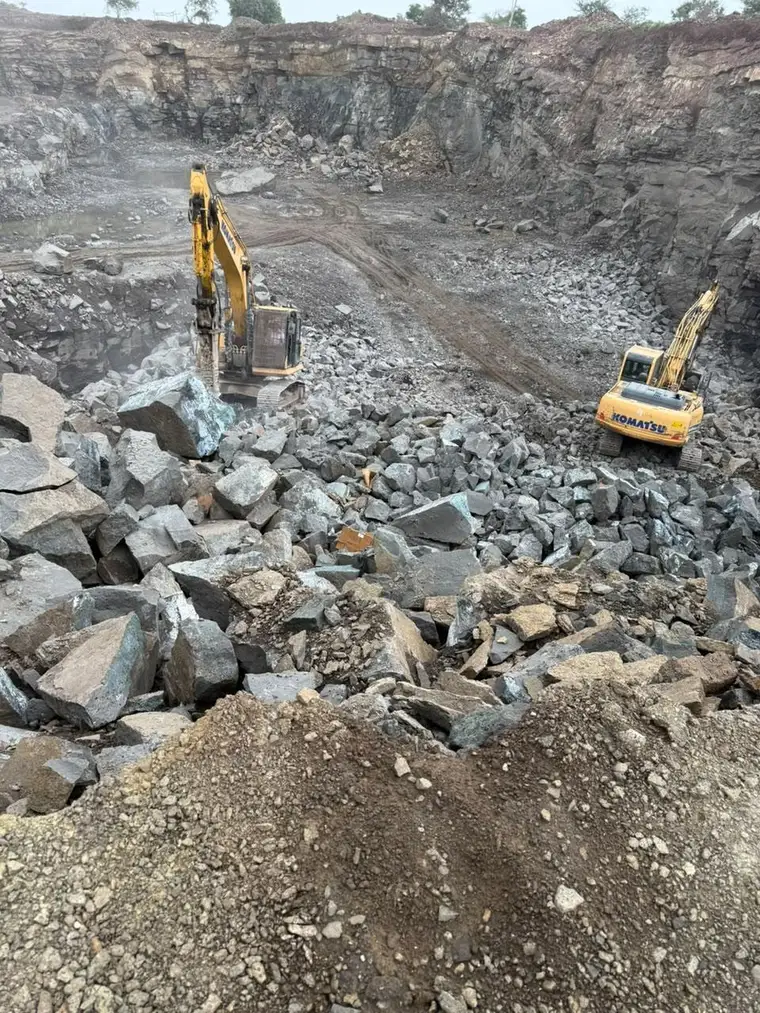
The bottom of the hole is where the rock is most confined and the blast has its hardest job. If the hole has drifted back from the face, the burden down there is too large. The rock at floor level cracks without moving, a toe is left standing that the excavator cannot dig, and the ground between the hole and the face comes out in blocks.
If the hole has drifted towards the face, the burden is too small. The charge breaks out early through the thin rock in front of it, and energy that should have gone into breaking leaves as noise and throw. Insufficient burden at the front row, and inaccurate drilling, are both on the list of recognised causes of flyrock.
The same happens sideways along the row. Two holes that diverge leave a block between them too far from either. Two that converge spend their energy twice on the same rock.
Where deviation comes from
- An uneven bench floor. The rig is not level, or the collar starts on loose rubble and the bit skids before it bites.
- A rushed set-up. The angle is judged by eye and the direction is copied from the previous hole, mistake and all.
- Worn bits and rods. A bit worn on one side cuts off centre, and bent rods or slack couplings let the string flex.
- Jointing in the rock. A bit that meets an inclined joint or a hard band at a shallow angle is steered along it.
- Excessive feed force. Pushing harder to recover lost time bends the string, and a bent string drills a curve.
The last one is for whoever sets the day's target: a driller chased for metres finds them by leaning on the feed.
How it is controlled
- The bench is cleaned and levelled before marking, so the rig can stand on the mark.
- Collars are surveyed and painted, and each hole is drilled on its mark or the move is recorded.
- Angle and direction are checked with an instrument at every set-up, not carried over from the last hole.
- The hole is collared gently, with low feed until the bit is established in sound rock.
- Bits and rods are changed before they are worn out.
- Finished holes are measured before charging: depth taped, blockages found, and on a deep or irregular face the true burden established by survey.
The measurements go to the shotfirer, who decides what to do about a hole that is out. Often the right answer is to drill it again. A redrilled hole costs a few metres. An accepted bad hole costs far more, somewhere else. On our drilling work deviation is measured, not assumed, because a hole nobody checked is a hole that will surprise the shotfirer.
What oversize costs downstream
Oversize is rock too large for the primary jaw. Each piece is handled again: set aside by the excavator, broken with a hydraulic rock breaker, then loaded a second time. That is a machine and an operator producing nothing new, and the cost never appears against drilling.
Pieces that get past the sorting bridge across the hopper or the jaw opening, and the plant stops while they are cleared. One of our 250 TPH three-stage plants is rated for up to 1,00,000 MT a month on two shifts, and it only gets there by running its hours. Hours lost to a bridged jaw do not come back. That is why the drill-and-blast step of a mining operation is designed around the fragmentation the crusher wants: oversize costs more at the hopper than it saves at the face.
So if a muck pile shows boulders in a regular pattern, or a toe in the same place bench after bench, look at the drilling before blaming the explosive. Burden, spacing and sub-drilling sets out the design the holes should match, and fragmentation and crusher output follows the result into the plant.
Standards and sources
- Offset figures: trigonometry (depth multiplied by the tangent of the angular error), calculated for this article
- Published studies of flyrock in opencast blasting: insufficient burden, inaccurate drilling and hole deviation among the recognised causes
- Plant output and drilling practice: SM Infra's own operating record
Your contract and its technical schedules override anything written here. Check the clause before you build to it.